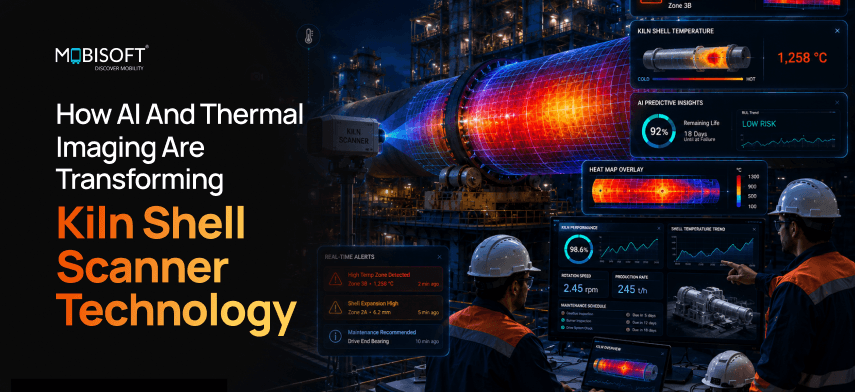
A rotary kiln shell running at 1,450°C with a failing refractory lining? That's one of the most expensive nightmares in industrial manufacturing. Consider this: a cement plant hit with a 24-hour unplanned shutdown can bleed $500,000–$1.5 million in lost production alone. And that's before you factor in emergency repairs, replacing the refractory, or the domino effect on your entire schedule. For decades, refractory failure detection meant relying on operator experience, walking around with clipboards for manual checks, and hoping those basic temperature alarms would actually help. The arrival of AI-driven analytics, paired with high-resolution thermal imaging kiln refractory monitoring, has changed the game completely. Now you're not just reacting to problems. You're predicting those days or even weeks before catastrophe hits.
The Rotary Kiln Challenge: Why Shell Monitoring Is a Safety and Economic Imperative
What a Rotary Kiln Operates Under
Let's be clear about what we're dealing with. Rotary kilns aren't just another piece of equipment. They're the thermal heart of cement production, lime processing, alumina refining, iron ore pelletising, and hazardous waste incineration. A typical cement kiln runs about 60 to 100 metres long. Maybe four to six metres in diameter. It spins at one to five revolutions per minute while operating at temperatures between 1,400 and 1,500°C. Pretty brutal conditions. The steel shell itself couldn't survive that heat without protection. That's where the refractory lining comes in, usually 200 to 250 millimetres of high-alumina brick. It provides thermal insulation and structural shielding for the shell.
Why the Refractory Is the Kiln's Weak Spot
The refractory is also the kiln's weak spot. We've seen it over and over. It degrades constantly. Thermal cycling wears it down. Mechanical stress from rotation adds more pressure. Chemical attack from process gases eats away at it. Physical abrasion from the material bed grinds it bit by bit. Put simply, the lining takes a beating from every direction. As the lining thins, shell temperatures rise. When refractory fails, through brick spalling, joint opening, or zone collapse, the shell can reach temperatures that permanently deform or rupture the steel, creating a red-spot event. A red spot is not just a maintenance problem; it is a potential structural failure that can require the kiln to be shut down for weeks of emergency refractory replacement at costs ranging from $2 million to $10 million, depending on the affected zone.
Planned Replacement vs Emergency Red-Spot Repair
The difference between a planned refractory replacement and an emergency red-spot repair is approximately $8 million and 6 weeks of production time in a large cement plant. The difference between those outcomes is the quality of the kiln shell scanner technology deployed and whether it detects the precursors of failure before the failure occurs.
The Thermal Signature of Refractory Degradation
Understanding why the AI kiln monitoring system technology provides superior early warning requires understanding the thermal physics of refractory failure. When the refractory lining is healthy and full-thickness, the shell surface temperature is typically 200–350°C in normal operating zones. As the lining thins through degradation, the thermal resistance decreases, and the shell surface temperature rises. The relationship is approximately linear: a 20% reduction in lining thickness produces a measurable temperature increase that is detectable with modern thermal cameras before any visual indicator is apparent to operators.
| Refractory Condition | Shell Temp (Typical) | Detection Method | Time to Critical Failure |
| New/full thickness (200–250mm) | 200–280°C | Baseline thermal profile; normal operation | N/A |
| 10–15% thinning (worn lining) | 280–340°C | Temperature trending in the AI system; anomaly score rising | Weeks to months |
| 25–30% thinning | 340–400°C | Hotspot alert from AI system; operator notification | Days to weeks |
| 40–50% thinning | 400–500°C | High-priority alarm; maintenance intervention required | Hours to days |
| Brick spalling / imminent failure | 500–600°C+ | Critical alarm; shutdown consideration | Hours |
| Red spot (shell exposed) | 600–900°C+ | Emergency; immediate shutdown required | Imminent structural risk |
The Limitations of Traditional Kiln Shell Monitoring
Before AI thermal camera kiln shell hotspot detection became commercially available, kiln shell monitoring depended on a combination of approaches, each with significant limitations.
- Manual inspection: Operators walk beside the rotating kiln and look for discoloured or glowing patches on the shell at night. They catch only severe hotspots that are already critical, and the radiant heat puts them at risk.
- Fixed pyrometers: These are fast and cheap, but they measure a single point on a shell with thousands of square metres of surface. A hotspot that forms between two positions stays hidden until it grows big enough to see.
- Handheld cameras: Technicians scan the shell with LWIR cameras during maintenance access. Coverage beats fixed pyrometers, yet a failure that starts between scans stays invisible until the next one.
- Basic radiometers: Early continuous scanners alarmed on absolute temperature thresholds. They could not separate normal variation from real degradation, so they raised false alarms and missed genuine faults.
How AI-Enhanced Kiln Shell Scanners Work: The Complete Technical Architecture
Modern AI-enhanced kiln shell temperature monitoring systems bring together high-resolution thermal imaging hardware and machine learning analytics platforms. The result is a continuous, intelligent monitoring capability that does more than just measure temperature. It actually predicts refractory health. To evaluate or deploy these systems effectively, you really need to understand how they're built. That means looking at the sensors, the data pipeline, the AI models underneath it all, and the operator interface on top.
The Thermal Imaging Hardware Layer
| Component | Specification | Function | Why It Matters |
| LWIR thermal camera | 7.5–14μm; 640×480 to 1280×1024 px; 0.1°C NETD | Captures a full thermal map of the kiln shell per scan pass | Higher resolution detects smaller hotspots; 0.1°C NETD enables early-stage anomaly detection |
| Scanning mechanism | Linear or area scan; 50–200Hz scan rate | Generates a 2D unwrapped thermal image of the full shell per rotation | Higher scan rates produce more thermal data points per rotation for AI input |
| Encoder interface | Rotary encoder; 0.01° angular resolution | Synchronises thermal acquisition with kiln rotation position | Enables precise geo-referencing of every temperature measurement, essential for change detection |
| Environmental housing | IP65/IP67; water cooling or air purge; EMI shielding | Protects the sensor in hot, dusty, vibration-heavy environment | Kiln environments are among the harshest in industry; sensor reliability is the primary hardware differentiator |
| Visible light camera | 2–5 megapixel; aligned with thermal camera FOV | Visual context for thermal anomalies; documentation | AI uses visible image correlation to distinguish process material on the shell from genuine hotspots |
| Reference temperature sources | Calibrated blackbody targets; ambient sensor; emissivity correction database | Compensates for emissivity variation and ambient temperature changes | Without emissivity correction, temperature errors of 20–50°C are common; AI cannot reliably detect anomalies at this error level |
The Data Pipeline: From Pixels to Predictive Intelligence
Preparing the Thermal Frames
Raw thermal frames from the LWIR camera pass through a structured processing pipeline before the AI models ever see them. The pipeline begins with image acquisition at 50–200Hz, with a rotary encoder providing the rotation position for each frame. Raw frames then undergo emissivity correction, ambient temperature compensation, geometric correction for kiln curvature, and noise filtering.
The corrected frames are then unwrapped: the 3D cylindrical surface of the kiln is mapped to a 2D thermal image where each pixel is geo-referenced to a specific axial position and circumferential angle. Thermal maps from multiple rotations are averaged to reduce noise, with statistical outliers from process material such as clinker and dust removed in the process.
From Clean Thermal Maps to Operator Alerts
Here's how the workflow typically goes. Once the system cleans and geo-references those thermal maps, they get passed to the industrial thermal scanner's AI analytics engine. That's where machine learning models spot deviations from zone-specific baselines and calculate anomaly scores. Time-series analysis then takes over, driving trend charts and offering up estimates of remaining life. The data analytics system generates multi-level alerts based on anomaly scores, temperature thresholds, and trend slopes. Those alerts appear on the operator dashboard and get pushed out to your plant DCS, SCADA, and EAM systems. It sounds complicated, but the idea is simple: catch the problem early, before the kiln forces your hand.
The AI Analytics Engine: Machine Learning Models in Kiln Shell Scanners
The most significant advancement in kiln shell scanner technology is not the improvement in thermal sensor resolution, though that has been significant. It is the application of machine learning analytics to the thermal data stream. AI transforms raw temperature measurements into actionable intelligence by learning the normal thermal signature of a specific kiln, identifying statistically anomalous deviations, and predicting the future trajectory of developing hotspots.
The Machine Learning Models Used in Kiln Shell Monitoring
Several distinct model types work in combination within a modern AI kiln monitoring system.
Baseline Thermal Modelling With an Autoencoder
Baseline thermal modelling uses an unsupervised autoencoder. It learns the kiln's normal thermal signature. That signature depends on feed rate, fuel type, rotational speed, and even ambient temperature. Different conditions give different readings. The model flags anything that strays from this learned baseline. Not from some generic average. That last part matters because it kills false alarms. Normal operational variation won't trick the system.
Anomaly Scoring With Isolation Forest or OCSVM
Each pixel and shell zone gets a score. The score measures deviation from that zone's own baseline. Imagine a zone that usually runs at 320°C. It alarms at 360°C. Another zone normally runs at 280°C. It triggers earlier for the same 40-degree jump. That per-zone sensitivity is the secret to early kiln shell hot spot detection.
Hotspot Growth Prediction With LSTM
Hotspot growth prediction uses LSTM or a time-series RNN. The system watches how fast the temperature rises per zone. It then predicts when a hotspot will hit critical levels. For example, "At this rate, Zone 7B reaches 450°C in about 36 hours." That kind of estimate helps you schedule maintenance properly.
Refractory Wear Pattern Classification With CNN
Refractory wear pattern classification relies on a CNN. It looks at spatial patterns of thermal anomalies. Then it identifies the failure type. Maybe a joint opening. Maybe brick spalling. Could be coating loss or ring formation. Each pattern looks different. Different failure modes carry different urgency profiles and require different remediation approaches.
Coating and Accretion Detection
This model identifies coating buildup, ring formation, and accretion patterns from thermal signatures. This prevents false alarms from coating buildup being confused with refractory failure, which is a common and expensive source of alert fatigue in threshold-based systems.
Multi-Variable Correlation With Gradient Boosting
Gradient boosting correlates thermal data with process variables including feed rate, fuel rate, kiln speed, and inlet/outlet temperature. This reduces false alarms by 30–50% compared to temperature-threshold-only systems by distinguishing operational causes of temperature change from structural causes.
Transfer Learning: Accelerating Deployment Across Similar Kilns
A significant practical challenge in AI-based rotary kiln predictive maintenance is the time required to train baseline models on a new kiln, typically 4–12 weeks of normal operation data before the system has sufficient baseline knowledge to detect anomalies reliably. Transfer learning addresses this by pre-training models on datasets from similar kilns of the same diameter, process type, and refractory specification, then fine-tuning on the new kiln's specific data.
The impact is substantial. A system deployed on kiln number five in a fleet of similar kilns can begin producing useful anomaly scores within 1–2 weeks rather than 8–12 weeks, because the pre-trained model already understands the thermal behaviour characteristics of kilns of that type. The fine-tuning period then learns kiln-specific patterns, such as a historically warm zone near a support tyre or the thermal signature of a specific feed composition, that distinguish this kiln from the generic model.
AI Performance Benchmarks: What Leading Systems Achieve
| Performance Metric | Leading AI System | Pre-AI Threshold System | Significance |
| True positive rate | 96–98% of genuine failures detected | 70–80% | 4–30% improvement means fewer failures reach red-spot stage |
| False positive rate | 2–5% of alerts are false positives | 15–30% | Lower false alarm rate drives operator compliance with alerts |
| Early warning lead time | 48–96 hours before critical temp | 4–12 hours before threshold breach | 48–84 hours of additional lead time for maintenance scheduling |
| Min. detectable anomaly | 2–5°C above zone-specific baseline | 15–30°C above global threshold | Order-of-magnitude sensitivity improvement; detects gradual thinning earlier |
| Hotspot localisation | ±50mm axial; ±2° circumferential | ±500mm for fixed pyrometer arrays | Precise localisation enables targeted inspection during planned stops |
| Failure type classification | 85–92% correct classification | Not applicable | Classification enables a prioritised response based on failure mode |
Industry Applications: Where AI Kiln Shell Scanners Are Being Deployed
AI-enhanced kiln shell scanner technology is deployed across every major industry that uses rotary kilns for high-temperature processing. While the underlying technology is the same, the specific monitoring challenges, process parameters, and economic stakes differ significantly between industries.
Application by Industry
The following overview covers how kiln shell temperature monitoring requirements and AI system benefits vary by sector.
Cement Clinker Production (1,400–1,500°C)
Kilns are 4–6m in diameter and 60–100m long, rotating at 1–4 rpm. The main challenge is telling clinker coating loss apart from true refractory degradation. Hot meal ring formation and alkali-related brick damage add to the problem. AI separates coating variation from structural refractory failure and catches ring formation before it disrupts the process. Operators can then re-establish coating through operational adjustments.
Lime Calcination (950–1,250°C)
Kilns are smaller (2–4m diameter; 30–60m long) and refractory wear is faster than in cement due to more abrasive feed. Shell flexure from product segregation and tyre migration is an additional concern. Continuous AI monitoring of higher-wear zones and tyre slip detection from thermal signature changes are the primary benefits.
Alumina Calcination (900–1,100°C)
Alumina kilns are similar in size to lime kilns, often longer. Product build-up patterns and ring formation in specific zones are the dominant challenges. AI provides ring growth trend monitoring with estimated days to process impact.
Iron Ore Pelletising and Induration (1,250–1,350°C)
These are large-diameter kilns (5–7m; 60–120m long) with multiple temperature zones. Multi-zone thermal management and tyre area monitoring for bearing and tyre overheating are the key applications of AI monitoring.
Hazardous Waste and Secondary Fuels (800–1,200°C)
Variable feed creates complex and unpredictable thermal patterns. AI models trained on waste-specific thermal signatures can separate genuine anomalies from process variation and provide audit trails for regulatory compliance reporting.
Titanium Dioxide Production (900–1,100°C)
Corrosive process atmospheres cause faster refractory degradation than in standard kilns. AI models account for accelerated degradation patterns and shorter early warning windows compared to less corrosive processes.
The Cement Industry: The Largest Deployed Base
Cement manufacturing represents the largest installed base for kiln shell scanner technology globally, with approximately 4,200 cement kilns operating worldwide and an increasing proportion equipped with continuous thermal monitoring systems. The economic stakes are particularly compelling in cement. A typical cement kiln produces 1,500–5,000 tonnes per day of clinker worth $30–$60 per tonne, meaning a single day of unplanned downtime costs $45,000–$300,000 in lost production alone, before accounting for maintenance costs.
AI thermal camera kiln shell hotspot detection has added specific value in cement beyond basic hotspot detection.
- Coating loss detection: Makes the clinker coating's condition thermally visible, and its loss is a detectable precursor to accelerated refractory wear.
- Ring formation monitoring: Catches build-up rings before they cause process disruption.
- Fuel substitution monitoring: Lets AI models trained on mixed-fuel operation correctly distinguish fuel-related thermal changes from genuine refractory anomalies, a growing requirement as cement plants increase their use of alternative fuels.
Edge AI and IIoT Architecture: How Modern Kiln Scanners Are Deployed
The deployment architecture for AI kiln monitoring system solutions has evolved significantly in the 2023–2026 period. The original cloud-only model, where all AI processing ran on a central server, has been supplemented and in many cases replaced by edge AI architectures that process thermal data locally at or near the kiln. Only alarm states, trend summaries, and event data are transmitted to central systems. This evolution has been driven by the requirements of industrial environments: network reliability, latency, data sovereignty, and increasingly strict IT security policies.
The Three Deployment Architecture Models
Edge-Only Architecture
AI processing runs entirely on a local industrial PC or edge GPU at the kiln with no cloud dependency. Alarms and visualisation appear on a local operator terminal. Response latency is under 100ms. No internet connection is required, only a local LAN. This is best suited for plants with poor connectivity, high-security environments, and operations with strict data sovereignty requirements. This architecture delivers the core promise of edge AI kiln monitoring with no internet dependency.
Edge Plus Cloud Hybrid Architecture
Edge AI handles real-time anomaly detection and local alarming. The cloud receives thermal trend data, trains updated models, and runs fleet-level analytics. Edge response stays under 100ms. Cloud analytics run on a cycle of minutes to hours. Local alarming continues if the connection drops. Most industrial plants use this setup today because it combines fast local response with cloud-scale analytics and model improvement.
Cloud-Primary Architecture
Thermal images are streamed to the cloud for AI processing, and alarms are returned to the local system. Latency is 200ms–2 seconds, depending on network conditions. This requires a reliable high-bandwidth connection and is best suited for plants with excellent connectivity and a preference for centralised IT management.
Integration with Plant Systems: SCADA, DCS, and EAM
The value of rotary kiln predictive maintenance data is maximised when it is integrated with the plant's control and maintenance management systems, a core step in any serious digital transformation initiative. Modern AI kiln shell scanner systems provide the following integration pathways.
- DCS/SCADA integration (OPC UA / Modbus TCP): real-time alert states, zone temperatures, and anomaly scores are published as OPC UA nodes or Modbus registers that the plant DCS can read and display on control room operator screens. Kiln shell alerts appear in the same interface operators use for all process control, not on a separate specialist screen that may go unmonitored.
- Enterprise Asset Management (SAP PM, IBM Maximo): When the AI system generates a maintenance recommendation, it can automatically create a maintenance notification in the plant's EAM system with the zone location, temperature data, and AI confidence score attached as evidence. This closes the loop between monitoring and maintenance action.
- Historian integration (OSIsoft PI, AspenTech IP21): long-term thermal trend data stored in the plant historian enables retrospective analysis of refractory life cycles, comparison between campaigns, and calibration of refractory life prediction models with actual failure history.
- AI-to-AI integration: In the most advanced deployments, the kiln shell scanner AI system shares data with process optimisation AI systems, allowing process control to factor refractory health into combustion adjustments. A kiln with a developing hotspot in a specific zone can be operated with reduced intensity in that zone while maintaining overall production targets.
The Economic Case: ROI of AI Kiln Shell Scanners
The economic case for rotary kiln predictive maintenance technology is among the most straightforward in industrial AI. The cost of a single prevented unplanned shutdown typically exceeds the entire system investment, making the ROI calculation a matter of estimating failure frequency rather than debating whether prevention is worthwhile.
The Cost Components of a Rotary Kiln Red-Spot Event
The following cost ranges apply to a large cement plant experiencing a red-spot event.
- Lost production: $250,000–$1,500,000 per day. Varies by kiln capacity (1,500–5,000 tpd), product value, and market conditions.
- Refractory materials: $500,000–$3,000,000. Includes emergency supply premium, expedited shipping, and full affected zone replacement.
- Emergency labour: $200,000–$800,000. Covers 24/7 emergency crews at premium rates using specialised refractory installers.
- Mechanical repairs: $100,000–$2,000,000+. Shell deformation or tyre damage from a severe red-spot event; worst case requires shell section replacement.
- Investigation: $50,000–$200,000. Covers engineering investigation, compliance reporting, and HAZOP review if required.
- Total range: $1,100,000–$7,500,000+. A severe event with shell damage reaches the upper range; a contained hotspot caught before structural damage falls at the lower range.
AI Kiln Scanner System Cost and ROI Model
The following figures cover a typical AI kiln shell scanner technology deployment at a large cement plant.
- System: $120,000–$350,000 for hardware and software. Varies by kiln size, number of monitoring zones, and software licence model.
- Installation: $30,000–$80,000. Covers mechanical installation, electrical integration, DCS/SCADA integration, and staff training.
- Maintenance: $15,000–$40,000 per year. Covers AI model updates, software upgrades, and technical support.
- 5-year cost: $225,000–$630,000 total ownership cost.
Set against those ownership costs, the ROI drivers are compelling.
- Prevented shutdown: $1,100,000–$7,500,000 per unplanned shutdown avoided.
- Planned conversion: $300,000–$1,200,000 per event converted from unplanned to planned downtime.
- Campaign life: $100,000–$500,000 per year from AI-optimised operational adjustments that protect the lining.
- Payback: 3–18 months. Most deployments see payback within 6–12 months.
Published Industry Results
| Plant / Region | Kiln Type | Result | Timeframe |
| Multiple European cement plants (FLIR / Thermo-Vision) | Grey cement, 3,000–4,500 tpd | 40% reduction in unplanned downtime; 2–3 additional refractory campaign months per year | 2–3 year measurement periods |
| Australian lime plants (KilnCheck AI) | Rotary lime, 500–1,000 tpd | 72-hour average warning before critical hotspot; zero red-spot events in 24 months post-deployment | 2 years post-deployment |
| North American cement plant (AI specialist) | Cement, 4,500 tpd | Single prevented shutdown in Year 1, paid for entire system 3x; 6 emergency interventions avoided via coating loss detection | 18 months |
| South East Asian cement fleet (multi-kiln) | 4 kilns, mixed capacity | $4.2M estimated savings in Year 1 from avoided shutdowns and extended lining campaigns | Year 1 post-deployment |
Published results are from vendor case studies and industry conference presentations. Independent third-party verification of all claims has not been uniformly conducted. Plant-specific results vary based on operating conditions, initial monitoring state, and baseline failure frequency.
Generative AI and LLMs in Kiln Shell Monitoring: The Emerging Layer
While the core of kiln shell scanner technology is time-series anomaly detection and computer vision applied to thermal data, 2025–2026 has seen the first commercial deployments of generative AI and large language model (LLM) interfaces on top of the underlying monitoring infrastructure. These additions do not replace the core AI monitoring; they make its outputs more actionable and accessible.
LLM-Powered Natural Language Interfaces
From Raw Output to Operator Language
Kiln operators are process experts, not AI specialists. The output of an anomaly detection model, an anomaly score of 0.87 in Zone 7B with a 15°C above-baseline temperature, is meaningful to a data scientist but requires translation for a kiln operator who needs to know what it means, how urgent it is, and what to do. LLM-powered natural language interfaces convert AI model outputs into operator-language recommendations.
For example, a raw output of "Zone 7B: anomaly_score=0.87; delta_T=+15.3°C; rate=+0.8°C/hr; pattern_class=GRADUAL_THINNING; TTF_estimate=62hrs" becomes the following operator summary: Zone 7B Alert Refractory Thinning Detected. Temperature in this zone has been rising at 0.8°C per hour for the past 18 hours, reaching 15°C above its normal baseline. The thermal pattern suggests gradual refractory wear rather than sudden damage. At the current rate, this zone will reach the action threshold in approximately 62 hours. Recommended action: Schedule a detailed inspection of Zone 7B during the next planned stop. If the rate of increase accelerates above 1.5°C/hr, consider reducing flame intensity in this zone as a protective measure. Next review: 6 hours.
Separating Urgent Alerts From Operational Noise
By contrast, a lower-priority signal, such as coating variation following a fuel mix change, is summarised as a low-priority informational note. The LLM explains that the elevated temperature correlates with the recent fuel adjustment and will self-resolve within 4–8 hours as the coating re-establishes, with no action required. This distinction between urgent structural alerts and operational noise is where LLM interpretation delivers direct operational value.
AI-Assisted Maintenance Planning
Generative AI systems connected to the rotary kiln predictive maintenance platform can assist maintenance planners by synthesising thermal data, historical maintenance records, and operational schedules to produce maintenance recommendations with estimated materials and duration.
A representative output reads as follows: "Based on current thermal profiles and historical wear rates for this kiln, the following interventions are recommended at the next planned stop scheduled in 18 days. Priority 1: Zone 7B refractory inspection and likely brick replacement (4–6 bays estimated; 8 hours labour; 2.4 tonnes VDZ35 brick). Priority 2: Zone 4A joint sealing inspection (no brick replacement anticipated; 2 hours labour). Priority 3: General condition survey of zones 1–3 and 8–10 (within normal parameters but approaching mid-campaign inspection threshold). Total estimated stop extension: 12 hours above minimum maintenance allocation."
This type of AI-synthesised maintenance brief, combining thermal data with EAM history, refractory specifications, and schedule constraints, represents a significant reduction in maintenance planning time and a measurable improvement in materials pre-positioning accuracy.
The Kiln Shell Scanner Vendor Landscape and System Selection Guide
The kiln shell scanner market has grown significantly with AI integration, with a range of vendors offering systems from basic continuous thermal scanning to fully AI-integrated predictive platforms. Understanding the vendor landscape and the selection criteria helps plants choose a system appropriate to their specific monitoring requirements and operational context.
The Vendor Category
Established Industrial Thermal Imaging Vendors
FLIR Systems / Teledyne, Micro-Epsilon, and Raytek / Fluke offer moderate AI capability, with anomaly detection and trending added to existing product lines. Systems are deployed primarily on-premise with some cloud connectivity. Best suited for large plants wanting to integrate with existing FLIR or Raytek infrastructure.
Specialist Kiln Monitoring Vendors
KilnView, Faber Burner, and CEMA offer high AI capability within their specific domain, with deep kiln expertise and models trained on large kiln dataset portfolios. Systems are deployed via edge plus cloud hybrid with field service support from kiln specialists. Best suited for plants wanting a deep cement or lime process context in their monitoring system.
Industrial AI Platform Vendors
Seeq, Aspen Technology, SparkCognition, and Uptake apply very high general industrial AI capability to kiln data, though potentially with less specific kiln or refractory model depth. Cloud-primary deployment integrates with existing historians such as OSIsoft PI. Best suited for large multi-site operations wanting fleet-level analytics across all assets, including kilns.
Specialist Startup AI Kiln Vendors
Newer entrants (2020–2025) are AI-native from design rather than retrofitted, potentially offering the highest AI sophistication in the category. Typically, cloud plus edge hybrid on a SaaS model. Best suited for plants willing to work with newer vendors seeking the most advanced AI capability and often the lowest total cost of ownership.
System Selection Criteria
AI Model Performance (High Weight)
Compare true positive rate, false positive rate, minimum detectable temperature delta, and early warning lead time. Use validated performance data from comparable kilns. Ask vendors for third-party validated data from a similar kiln type. Also ask for false positive rates during the first three months, before baseline training is complete.
Domain Expertise in Your Specific Process (High Weight)
Check that the vendor has reference sites in your industry and kiln type. Cement, lime, alumin, and waste processing each have different thermal imaging kiln refractory monitoring needs. Ask how many kilns of your process and size they monitor. Request introductions to two maintenance managers at comparable sites.
Integration Capability With Existing Plant Systems (High Weight)
Confirm OPC UA, Modbus, DCS, and historian integration, plus SAP PM or Maximo work order creation. Ask the vendor to demo a live integration with your DCS brand and EAM system. Ask who is responsible for the integration work.
Edge AI Capability and Network Independence (Medium-High Weight)
Confirm the system gives zone-specific remaining life estimates and exports campaign data for post-campaign analysis. Ask for a sample refractory campaign report from a comparable site. Ask for historical TTF prediction accuracy data.
Refractory Life Prediction and Reporting (Medium Weight)
Confirm the system produces zone-specific remaining life estimates and supports export of campaign data for post-campaign analysis. Ask for a sample refractory campaign report from a comparable site and for historical TTF prediction accuracy data.
Training Time to Reliable Baseline (Medium Weight)
Confirm the minimum data collection period before the AI model produces reliable anomaly scores. Ask what alarm logic applies during training, while the baseline model is still incomplete.
Total Cost of Ownership and Commercial Model (Medium Weight)
Ask whether AI model improvement is included in the annual maintenance fee. Ask how often anomaly detection models are updated and how updates reach edge systems.
Implementation Guide: Deploying an AI Kiln Shell Scanner Successfully
The technical capability of an AI kiln monitoring system is only realised when the deployment is executed correctly. The most common reasons that kiln shell scanner systems underperform their specification are not technical failures. They are implementation failures: poor sensor positioning, inadequate operator training, insufficient integration with maintenance processes, and failure to maintain the AI model through operational changes.
The Deployment Phases
Phase 1: Site Survey and Design (2–4 Weeks)
Kiln dimensional survey; sensor foundation and housing design; electrical and network routing; DCS/SCADA integration design; EAM integration design. Success criterion: signed-off mechanical and electrical design drawings with integration architecture approved by plant IT and OT teams.
Phase 2: Hardware Installation (3–7 Days, During Planned Stop)
Sensor housing installation; cable routing; encoder installation; edge computer installation; initial electrical commissioning. Success criterion: thermal camera producing live images with encoder signal confirmed, and the edge computer communicating with the sensor.
Phase 3: Software Commissioning and Calibration (1–2 Weeks)
Kiln geometry configuration; emissivity calibration; reference temperature source configuration; initial threshold alarm setting; DCS tag mapping. Success criterion: all shell zones correctly mapped, temperature readings validated against an independent pyrometer reference, and basic threshold alarms tested end-to-end to DCS.
Phase 4: AI Baseline Training (4–12 Weeks)
The system operates in learning mode, collecting normal operation data across the full range of operating conditions. Success criterion: AI anomaly scores are stable and sensible during normal operation, with a false alarm rate below 10% during the training period.
Phase 5: AI Model Activation and Validation (2–4 Weeks)
Full AI anomaly detection runs in parallel with traditional alarms during validation. Success means the AI system detects all real anomalies during validation, the false positive rate stays below 5%, and the plant team trusts the alarms.
Phase 6: Integration Completion and Handover (1–2 Weeks)
The team activates EAM work order integration, confirms historian integration, completes operator training, and delivers the documentation. Success means plant operators can use the AI dashboard, understand alert classifications, and start a maintenance response from the system. All integrations must be live and tested.
The Most Common Implementation Mistakes
Sensor Positioning Without Considering Field of View Obstructions
Kiln shells have support tyres, riding rings and tyre pads at fixed axial positions. These cast thermal shadows in the scanner's field of view and can hide adjacent refractory zones. Account for them in the scanner positioning design. Either document them as blind zones or add a second sensor to cover them.
Skipping Emissivity Calibration
Rotary kiln shells change emissivity continuously as the steel oxidises, dust accumulates, and paint degrades. Without regular emissivity calibration or a model that corrects for emissivity variation, temperature measurement errors of 20–50°C can produce both missed detections and false alarms. Emissivity calibration using a contact thermocouple reference should be performed at commissioning and after any kiln stop where the shell is cleaned or inspected.
Treating AI Training as a Passive Period
The AI baseline training period of weeks 1–12 requires active management. Label and exclude abnormal data from baseline training. Examples include reduced production, a known temporary hotspot, or a fuel mix change. A model trained on abnormal conditions produces unreliable refractory failure detection AI anomaly scores.
Poor Integration With Maintenance Decisions
A kiln scanner can produce excellent alerts. If no one acts on them, the scanner adds little value. It also gives you false confidence that the kiln is covered. Design the link to maintenance on purpose. Decide who receives each alert and who makes the repair decision. Set the response protocol for every alert level.
The Future of AI Kiln Shell Scanner Technology: 2026–2030 Outlook
The kiln shell scanner technology market is evolving rapidly, with several technologies and market trends that will reshape the capability and deployment model of these systems over the next 3–5 years. Understanding the trajectory helps plants make investment decisions that will remain relevant as the technology evolves.
Technology Trends of the Next Generation
Multi-Spectral and Hyperspectral Imaging
Systems today use long-wave infrared for thermal imaging and kiln refractory monitoring. They also add visible-light cameras for context. Next-generation systems are starting to include mid-wave infrared and near-infrared channels. These extra channels reveal chemical composition on the lining surface. They also show temperature distribution inside the refractory structure itself. Multi-spectral data helps AI models tell different failure mechanisms apart. Two failures might look identical in long-wave infrared. But they look different in mid-wave or near-infrared. That difference is crucial.
Autonomous Drone Inspection Integration
Several vendors are now piloting autonomous drone integration. The drone works alongside the fixed shell scanner system. The fixed scanner provides continuous monitoring every minute of the day. When it finds a suspicious zone, something interesting happens. It automatically triggers a drone inspection. The drone flies in close for high-resolution thermal and visible images. You get a much better look at that particular region. This combination provides continuous monitoring coverage without the spatial resolution limitations of fixed scanners while avoiding the cost of continuous high-resolution scanning across the entire kiln length.
Digital Twin Integration for Refractory Life Modelling
Thermal data from industrial thermal scanner AI analytics systems increasingly calibrates refractory digital twins. These are simulation models that predict refractory wear from thermal loads, material properties, and operating patterns. Combined with scanner data, a twin can do more than flag a developing hotspot. It can forecast that the current campaign ends in 47 days under current parameters, or in 64 days if specific operational adjustments are made.
Fleet-Level AI Learning
As the installed base of AI kiln scanners grows, vendors are building fleet-level learning models. These aggregate anonymised thermal data from hundreds of similar kilns to sharpen anomaly detection and wear prediction. A kiln installed in 2027 can draw on the learning of 500 similar kilns. Accurate baseline models then take days instead of months.
Tyre and Riding Ring Monitoring Expansion
Kiln monitoring is expanding beyond refractory in rotary kiln predictive maintenance. It now covers the mechanical condition of tyres, riding rings, support rollers, and thrust rollers. Their thermal signatures correlate with lubrication condition, alignment, and wear state. One thermal imaging infrastructure can then support a unified kiln health platform for both refractory and mechanical conditions.
AI and Thermal Imaging in Kiln Shell Scanning: The Decisive Shift
The integration of AI analytics with high-resolution thermal imaging kiln refractory monitoring has transformed kiln shell scanner technology from a basic alarm system into a predictive intelligence platform. Moving from fixed-threshold alarms to machine-learning anomaly detection is a big deal. Moving from zone-average temperatures to pixel-level baseline models is also huge. This is not just a small improvement. It fundamentally changes what monitoring can detect. It changes how early you can detect it. And it changes what actionable information reaches your maintenance and operations teams.
The economic case is compelling and increasingly well-documented. A single prevented unplanned shutdown pays for the system multiple times over. The safety case is equally clear. The alternative to AI kiln monitoring system deployment is not better human observation. It is the acceptance that some failure modes will not be detected until they are already in a critical state, with the attendant risks to equipment, personnel, and production continuity.
For plants evaluating rotary kiln predictive maintenance technology in 2026, the key questions have moved beyond whether AI thermal imaging works, since the evidence for that is established. The relevant questions now are which system best fits the specific process, the IT architecture, the maintenance workflow, and the integration requirements. The selection framework and vendor evaluation criteria in this guide provide the structure for answering those questions rigorously.
The directional trajectory, covering edge AI processing, multi-spectral sensing, digital twin integration, and fleet-level learning, points toward kiln monitoring systems that are not just more sensitive but genuinely intelligent about the specific kiln they are monitoring. They learn from every campaign and every failure mode to become more accurate and more useful over time. The plants that invest in industrial thermal scanner AI analytics infrastructure today are building a predictive maintenance capability that will compound in value as the models improve and as the operational history deepens.
About Mobisoft Infotech
Mobisoft Infotech designs and builds industrial IoT platforms, edge AI systems, and predictive maintenance applications for heavy industry, including thermal monitoring data pipelines, AI anomaly detection systems, and plant operations dashboards. Our industrial AI practice bridges the gap between specialist sensing hardware and actionable operational intelligence for cement, lime, mining, and process industries.
Frequently Asked Questions
Can Mobisoft Infotech add AI analytics to my existing thermal scanner?
Yes, if your camera exposes radiometric data through GigE Vision, RTSP, or an SDK. We install an edge computer, connect the encoder feed, and run industrial thermal scanner AI analytics beside your current system. You can keep your hardware. You gain anomaly scoring, trend forecasts, and DCS alerts.
How often should I retrain the model after a kiln reline?
Retrain after every full reline, because new brick changes the thermal baseline. We run the model in learning mode for one to two weeks and apply transfer learning from earlier campaigns. Minor repairs need only recalibration. This keeps rotary kiln predictive maintenance accuracy stable across campaigns.
How do you reduce alert fatigue after go-live?
We tier alerts into information, warning, and critical levels. Each alert shows its zone, score, and contributing variables. Operators mark alerts as valid or false, and we feed those labels into retraining. Suppression rules cover known events such as fuel changes, which keeps kiln shell hot spot detection trusted.
What process data do you need to train a kiln model?
Start with shell thermal maps. Add historian tags for feed rate, fuel rate, kiln speed, and inlet and outlet temperatures. Maintenance logs and past campaign records add context. Four to twelve weeks of normal operation builds the baseline for refractory failure detection AI models.
How does Mobisoft Infotech detect camera or sensor failures?
We monitor camera health through frame rate, encoder signal, housing temperature, and image quality checks. The platform flags drift, dirty lenses, and lost signals before they corrupt anomaly scores. You receive a separate maintenance alert for the sensor, which protects kiln shell temperature monitoring data quality.
This content is for informational purposes only and may include AI-assisted research or content generation. While we strive for accuracy, information may evolve over time. Readers are advised to independently verify critical information before making decisions.
Nitin Lahoti
Read more
Nitin Lahoti is the Co-Founder and Director at Mobisoft Infotech. He has 15 years of experience in Design, Business Development and Startups. His expertise is in Product Ideation, UX/UI design, Startup consulting and mentoring. He prefers business readings and loves traveling.
 Nitin Lahoti
 May 19, 2026